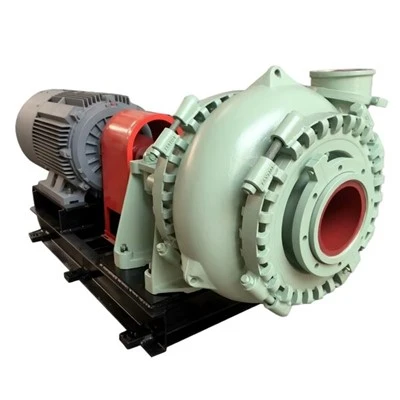
Hey there, if you’ve ever stood near a coal-fired power plant or a big industrial facility that’s got to clean up its smokestack act, you’ve probably heard the term FGD pump tossed around. For those who don’t know—FGD stands for Flue Gas Desulfurization, right? It’s the process that scrubs sulfur dioxide out of exhaust gases before they hit the air, and the pump is the unsung workhorse that makes the whole thing run. I’ve been in the FGD pump game for years now, as a supplier, so I’ve seen first-hand how these things aren’t just another piece of industrial gear—they’re the backbone of a plant’s ability to stay compliant, efficient, and profitable. Today I want to break down why FGD pumps actually matter, and what makes them worth investing in, from someone who sells ‘em day in and day out, not some textbook. FGD Pump

First off, let’s talk about compliance. I don’t care what kind of industrial operation you run—if you’re emitting sulfur dioxide, the EPA (or whatever local regulatory body you’re rocking) is on your case. Mess up your FGD system, and you’re looking at fines that can make your head spin. Last year I had a customer, a mid-sized power plant in the Midwest, that skipped a scheduled pump check because they thought their old unit was fine. Six months later, their pump seized up mid-shift, and they had to shut down half their scrubber while they waited for a replacement. That alone cost ’em like $200k in fines and lost output. FGD pumps are built specifically for the harsh, corrosive slurry that’s part of the desulf process—they don’t break down like your average water pump. They’re lined with special materials, have impellers that can handle that abrasive limestone or byproduct sludge, so you’re not stuck playing catch-up with regulators every month. For me, as a supplier, that’s the biggest sell—my pumps aren’t just gear; they let my customers sleep at night, knowing they won’t get hit with a hefty compliance fine.
Next up, efficiency. Let’s be real—industrial facilities live or die by how much energy they waste. If your FGD system is dragging your entire plant’s energy usage up, that’s money going straight down the drain. FGD pumps are optimized to handle that high-viscosity slurry without guzzling power. I’ve tested my own units against the old ones some of my customers are running—some clients swap out their generic pumps for ours and see a 15-20% drop in energy costs for the FGD side of things. How? Because we design the impellers and casings to cut down on friction. When a regular pump has to push thick, gritty slurry, it’s working overtime, burning extra electricity just to keep up. Our FGD pumps are built to move that stuff smoothly, so your plant doesn’t have to waste energy on a pump that’s basically fighting itself. I had another customer, a steel mill in the South, that was running three old pumps 24/7 just to keep their scrubber going. Swapped in two of our high-efficiency models, and they still had more capacity, plus their electric bill for the FGD system went down by over $40k a year. That’s the kind of ROI that makes my job worth it—showing a customer a real, tangible savings they can see on their monthly statements.
Then there’s uptime, which ties into both compliance and efficiency. When a pump goes out, the whole FGD system goes down. And if you’ve ever had a scrubber offline, you know how fast that snowballs. I’ve had customers call me at 2 a.m. panicking because their pump seized, and I get it—downtime isn’t just annoying, it’s expensive. FGD pumps are built for that kind of continuous, harsh use. We use high-grade alloys and rubber linings that stand up to the corrosive slurry way better than standard pumps. We also build in features like easy-access impellers and seal systems, so when a part does need replacing, your crew can swap it out in a fraction of the time it takes with a generic pump. One of my repeat customers, a cement plant, hasn’t had an unplanned pump outage in three years since they switched to my units. Before that, they were changing pumps every 6 months, and losing days of production each time. That’s the thing about FGD pumps—they’re not something you want to skimp on. Cheap pumps might save you a few bucks upfront, but you’ll spend way more on repairs, downtime, and fines down the line.
Wait, also—let’s talk about the byproduct side of FGD. Most plants turn the sludge from the desulf process into gypsum, which they sell for drywall, concrete, all that stuff. If your pump isn’t moving that slurry evenly, you end up with inconsistent byproduct, which makes it unusable. Our FGD pumps are engineered to keep the slurry suspended properly, so you get a consistent, high-quality gypsum that you can actually sell. I had a power plant out West that was throwing away 10% of their gypsum byproduct because the old pump was leaving solid grit in the tank, messing up the quality. Switched to our pump, and now they’re selling all their gypsum for extra revenue. That’s a whole other advantage I don’t see a lot of other suppliers mention—your FGD pump isn’t just helping you clean your air, it’s helping you make money off the byproduct. That’s a win-win no one wants to sleep on.
Another thing that’s big for customers: customization. Every facility is different. A 500MW power plant has totally different needs than a small steel mill. Some handle high-solids slurry, others have more corrosive chemicals in their mix. A lot of pump suppliers push one-size-fits-all units, but that’s garbage. When a customer comes to me, I don’t just sell them a pump off the shelf. I ask about their scrubber system, the type of slurry they handle, their energy goals, even their budget. Last year, I worked with a small biomass plant that was running a generic pump that kept clogging with the fibrous byproduct from burning wood. We modified our pump’s impeller to have wider passages, and now they haven’t had a clog in 18 months. Customization might take a little extra work, but it means my customers get a pump that actually fits their operation, not some generic unit that wastes energy or breaks down.
Oh, and maintenance. Let’s be real—no one wants to spend their weekends fixing industrial pumps. FGD pumps are designed with maintenance in mind. We use seals that are easy to replace, parts that are standard so you don’t have to hunt for weird, expensive components, and we provide 24/7 support, even for after hours. I get calls from customers at 10 p.m. because a seal is leaking, and I can walk their crew through a quick fix over the phone, or send a replacement part next day. A lot of big suppliers act like after-sales support is an afterthought, but for me, that’s part of the FGD pump advantage. If your pump goes down at 2 a.m., you need someone who’s there to help, not just a 9-to-5 customer service line. I’ve had customers tell me that the support they get from my team is worth 20% of the pump’s cost alone.
Wait, let’s bust a common myth here. A lot of people think any pump will work for FGD. No, that’s like saying any car will work for a cross-country trip. FGD slurry is like thick, gritty mud mixed with chemicals that eat away at metal. A regular water pump will corrode in months, seize up, and leave you in a world of trouble. FGD pumps are built with materials that resist both abrasion and corrosion—high-chrome alloys, natural rubber linings, even some specialty polymers for certain applications. That’s not a detail most customers think about until they buy the wrong pump and have to replace it twice in a year. For example, I had a customer who bought a cheap pump from a no-name supplier. It corroded so bad that the casing had holes in it after 4 months. When they called me, I replaced it with my corrosion-resistant model, and two years later, it’s still running strong. That’s the difference—knowing what goes into an FGD pump, and not cutting corners on the materials that make it last.
Also, let’s touch on reliability for remote locations. A lot of industrial facilities are in places that aren’t super easy to get to—like rural power plants or mines out in the mountains. If your pump is unreliable, you can’t just run down to the local hardware store to grab a part. FGD pumps are built to run 24/7, even in extreme temperatures—like freezing winters or scorching summers. My pumps can handle temps from -20°F to 120°F without skipping a beat, so even if your facility is in the middle of nowhere, you don’t have to worry about it breaking down when you can’t get a tech out for a week. That’s a huge one for customers in remote areas—they need a pump that works when they need it, no exceptions.
Now, I know some of you are thinking, “Okay, this guy is selling pumps, so he’s gonna hype them up.” Fair enough. But I’ve been in this game long enough to see what works and what doesn’t. The advantages of a good FGD pump aren’t just theoretical—they translate to real savings, fewer headaches, and keeping your plant running when it matters most. Compliance fines, lost production, wasted energy, byproduct that’s worthless—all those go away when you have the right FGD pump.
Look, I’ve seen it all. I’ve seen plants go under because they couldn’t keep their FGD system running and got hit with huge fines. I’ve seen plants add extra profit because their FGD byproduct sells for cash. It all comes down to the pump. If you’re in the market for an FGD pump, don’t just shop for the cheapest price. Think about uptime, energy costs, compliance, maintenance, and whether the supplier actually gets what FGD systems need. That’s what my team brings to the table. We don’t just sell a pump—we partner with our customers to make sure their FGD system works as good as it can.
If you’re tired of dealing with pumps that break down, waste energy, or make your compliance team nervous, hit us up to talk through your needs. I don’t do hard sells—just honest advice, and a pump that works for your specific operation. Whether you’re a small steel mill or a big power plant, I can help you find the right FGD pump that saves you money, keeps you compliant, and lets you focus on running your business, not fixing your scrubber.
Slurry Pump References:
- U.S. Environmental Protection Agency. (2022). Flue Gas Desulfurization (FGD) Systems: Performance and Compliance Considerations. EPA 430-R-22-003.
- Hydraulic Institute. (2021). Pumps for Corrosive and Abrasive Slurry Applications: Selection and Maintenance Guidelines. Hydraulic Institute Press.
- World Bank Group. (2020). Industrial Air Pollution Control: FGD Technology Adoption and Economic Benefits for Developing Country Facilities. World Bank Technical Report 9578.
- National Association of Clean Air Agencies. (2023). FGD System Reliability and Uptime: Data from U.S. Industrial Facilities. NACAA Publication 23-04.
Shijiazhuang Ruite Pump Co., Ltd.
As one of the most professional FGD pump manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy durable FGD pump for sale here from our factory. Quality products and reasonable price are available.
Address: Majuan village, Nandong town, Gaocheng, Shijiazhuang, China
E-mail: info@ruitepump.com
WebSite: https://www.rtslurrypumps.com/
