If you’ve ever stood on the floor of a manufacturing plant churning out everything from toy parts to automotive trim, you’ve probably glanced over a wall of injection molding machines and spotted a sleek, articulating arm gliding between the machine’s mold halves, grabbing a fresh part and setting it gently on a conveyor belt. That’s our injection molding robot—one of the most underappreciated workhorses of modern mass production—and today I’m breaking down exactly how it works, from the moment it’s programmed to the second it drops a finished part, all through the lens of what we’ve learned supplying these systems to manufacturers for over a decade. Injection Molding Robot
Let’s start with why this matters. Ten years ago, most injection molding operations relied on human workers to pull hot, freshly molded parts from machines, a process that was slow, risky (those parts come out at over 100°C, not to mention the sharp edges on things like plastic gear housings), and prone to error. A single missed shift would grind a production run to a halt, and repetitive stress injuries were a constant liability. When we first started selling our robots, the shift to automation felt like a big bet for a lot of clients, but now? 9 out of 10 of our repeat customers tell us their throughput is up 30% on average, and their workplace incident reports for mold floor tasks are down 75%. That’s the real payoff, but none of it would happen if we didn’t nail the mechanics and software that make these robots work.
Let’s get into the step-by-step, starting with the setup that happens before any part is molded. Every injection molding robot is custom-programmed for a specific machine and part, right out of the box. Unlike generic industrial robots that are built for 10 different tasks, our systems are calibrated to match the exact stroke, pressure, and cycle time of your injection molding machine. That means when the mold closes after injecting molten plastic, our robot’s arm doesn’t waste any time moving—its positioning system is already synced to the machine’s internal logic, called the machine’s PLC (programmable logic controller), which is the brain of every injection molding operation.
Here’s where the first key component comes in: the end-of-arm tool, or EOAT, that we build for every order. This isn’t just a clamp—it’s tailored to the part. For a flat plastic container lid, the EOAT uses a vacuum cup, which sucks gently against the smooth surface without scratching it. For a more complex part like a small automotive door trim, we might use a pneumatic gripper with custom rubber pads that fit the part’s curves, so it doesn’t deform the plastic while lifting it. We also integrate sensors into the EOAT—things like proximity sensors that check if the part is fully released from the mold, and temperature sensors that make sure we don’t grab a part that’s still too hot, which could warp it or damage the gripper. This is where our experience as suppliers really makes the difference; we don’t send a one-size-fits-all EOAT that causes delays. We build it to your exact part’s dimensions, and calibrate it so it only applies enough force to move the part, not break it.
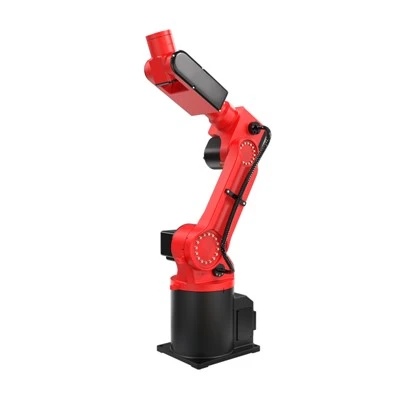
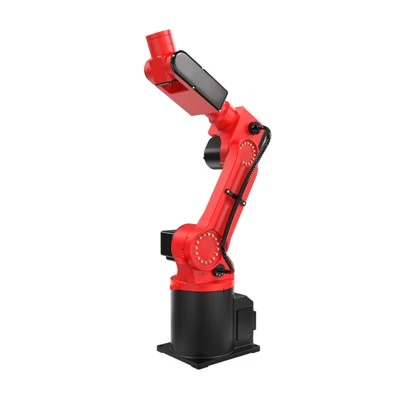
Now, let’s walk through the in-cycle sequence, step by step, just like the robot executes it. First, the injection molding machine completes its three main steps: it melts the plastic resin, injects it at high pressure into the mold, and then cools it until the part is rigid enough to handle. Once the cooling cycle is done, the mold opens—this is the signal the robot has been waiting for, thanks to that sync with the machine’s PLC. The arm, which is usually a six-axis articulated robot (think of a human arm with a shoulder, elbow, and wrist, each with full range of motion), moves from its parked position off to the side, straight to the mold’s cavity. The six axes let it reach around any obstructions in the mold, like ejector pins that push the part free once the mold opens, or the machine’s own clamping mechanism.
When the robot’s EOAT reaches the part, two things happen almost simultaneously: first, the ejector pins on the injection molding machine push the part slightly off the mold surface, so it’s easy to grab. Then, the EOAT’s sensors confirm the part is in place—no gaps, no misalignment. If the sensor doesn’t detect the part, the robot doesn’t try to grab it; it sends an alert to the plant’s control room, which is a huge upgrade over human operators who might not notice a missing part until the whole run is off. Once the part is secured, the arm retracts back, moving the part out of the way of the closing mold—this is critical, because if the robot moves too slow, the mold could close on the arm, causing thousands of dollars in damage and weeks of downtime. We program all our robots with a 0.2-second safety buffer here, a setting we refined after a client’s early setup had a mold close early, causing a $12,000 repair. That small, data-backed adjustment has saved our clients millions in repair costs over the years.
Next, the robot moves the part to its next destination. That could be a conveyor belt that carries parts to a packaging station, a secondary processing station where parts get trimmed or printed, or even a bin for rejected parts. This is where our robot’s positioning accuracy really shines—we program it to within 0.1 millimeters, so it drops parts exactly where they need to go, no more misaligned parts that jam the conveyor. For high-volume runs, like 10,000 toy action figures a day, we can also integrate vision systems into our robots. These small cameras snap a photo of each part right after it’s molded, comparing it to a digital blueprint we create during setup. If a part has a tiny flaw—like a air bubble or a missing detail—the vision system flags it, and the robot drops it into a separate reject bin, so only perfect parts make it to packaging. That cuts down on quality control labor by half for most of our clients, and reduces the number of defective parts that get shipped out.
Now, you might be wondering: what about safety? Manufacturing plants are tight, busy spaces, and people can’t be around the robot while it’s running. That’s why our systems come with a suite of safety features we design into every unit. First, the arm has force sensors built into each axis—if something (or someone) gets in its way, the sensor detects the sudden change in force, and the robot stops instantly, no crash. We also add light barriers around the robot’s work cell; if a worker steps past the barrier, the robot pauses immediately, instead of having a hard stop that could damage the arm or the part. A lot of smaller injection molding companies used to skip these features to save money, but we’ve seen too many accidents, so we make safety non-negotiable in every robot we sell.
Let’s talk about the difference between our robots and the generic ones you might find from other suppliers. A lot of injection molding robot vendors just take a standard industrial robot off the shelf and modify it to work with injection machines, but we engineer ours specifically for this application. For example, we build the arm materials to handle the heat and dust of a manufacturing floor—generic robot arms might get warped over time by the warm air from the injection molding machine, but our arms are made with high-strength aluminum alloys and coated with a heat-resistant layer that lasts for years. We also program our robots to adapt to small changes in production, like if a resin batch is slightly different, so the cooling time changes. Generic robots would follow a fixed cycle, even if the mold needs an extra second to cool, which can lead to warped parts. Our robots monitor the machine’s cycle time in real time, and adjust their own movement to keep up, so every cycle is consistent.
One of my favorite recent examples of this in action was a client that makes medical device components, like plastic syringes. They needed 99.9% perfect parts, because even a tiny flaw in a syringe’s plunger could lead to equipment failure. They were using a generic robot that missed about 2% of small flaws, so they switched to our system. In the first month, their defect rate dropped to 0.08%, and their throughput went up 25% because our robot was synced perfectly with their mold’s cycle. They told us it paid for the robot in 12 weeks, which is a return on investment we hear from almost every medical, automotive, and consumer goods client we work with.
Now, if you’re reading this and you’re running an injection molding operation, you might be thinking: “This sounds great, but how do I get started?” The process of integrating our robot is designed to be as smooth as possible, so you don’t have to shut down your whole production line for weeks. First, we come to your plant to do an on-site assessment: we measure your current injection molding machines, look at your part specifications, and talk to your team about your pain points—whether it’s slow cycle times, high defect rates, or safety concerns. Then, we build and program the custom robot for your operation, which usually takes 4-6 weeks. Once it arrives, our installation team is on-site for 2-3 days to set it up, sync it with your PLC, and train your operators. We don’t leave until your team is comfortable running the robot, and we offer 24/7 support for any questions or issues that come up.
At the end of the day, our injection molding robots aren’t just machines—they’re tools that help manufacturers do what they do better: make high-quality parts, keep their workers safe, and grow their business. We’ve been in this industry long enough to know that automation isn’t a one-size-fits-all solution, which is why every robot we supply is tailored to your specific needs, not off a catalog. If you’re ready to talk about how an injection molding robot could improve your throughput, cut defects, or make your workplace safer, we’re here to help. Reach out to our team to connect for a consultation and pricing.
Palletizing Robot References
- Groover, M. P. (2020). Automation, Production Systems, and Computer-Integrated Manufacturing. Pearson Education.
- International Organization for Standardization. (2018). Robots and robotic devices – Safety requirements for industrial robots. ISO 10218-1:2018.
- Injection Molding Association. (2022). The Role of Robotics in Modern Injection Molding Operations. Technical Report #IMR-22-04.
- Ratanavanichrojan, N., & Wannasen, A. (2021). Precision control of injection molding robots for small part production. Journal of Manufacturing Processes, 68, 1245-1253.
Robotic Technology (GD) Co., Ltd.
Robotic Technology (GD) Co., Ltd. is one of the most experienced injection molding robot manufacturers and suppliers in China, also supports custom service and one year warranty. Please feel free to wholesale CE approved injection molding robot for sale here from our factory. Contact us for quotation.
Address: Room 102, No. 30,Hengfeng 2nd Road,Daguo, Changping Town, Dongguan City,Guangdong,China
E-mail: admin@iroboticplus.com
WebSite: https://www.rb-tic.com/
