Hey everyone, it’s Jake here from the RS485 stack light team, and I get asked at least twice a week the same question: “Can an RS485 stack light be connected to a PLC?” If you’re an automation tech, plant manager, or hobbyist tinkering with your new line of production gear, this is probably crossed your mind too. Let’s cut through the confusion—no fancy jargon, just real talk from someone who’s sold these things for 6 years and has seen every win and misstep with these setups. RS485 Stack Light

First, let’s ground this in what we’re actually working with, because half the confusion comes from mixing up old-school relay-based stack lights with the smart RS485 ones we make. Back in the day, most stack lights were standalone: each color (red, yellow, green, maybe a buzzer) had its own wired connection back to the PLC, using discrete I/O pins. That meant if you wanted a 5-color stack light, you burned 5 PLC outputs, plus a ground, and you’d scramble for extra slots in your PLC rack faster than a new intern grabbing a coffee before a shift. Now, RS485 stack lights are smart—they’re on a serial network, not discrete wires. So yeah, they can connect to a PLC, but it’s not as plug-and-play as slapping a USB drive in your laptop. There are a few key things to get right, and I’m gonna walk through them like I’m troubleshooting a setup with a customer last week who thought he just needed a CAT5 cable and a power supply.
Let’s start with the basics: what’s RS485, anyway, for anyone who’s still translating tech acronyms in their head. RS485 is a balanced serial communication standard—think of it as a two-wire highway for data, not a bunch of one-lane roads. It can run up to 4,000 feet, support up to 32 devices on one network, and send commands instead of just turning a light on or off. That’s the big win with our RS485 stack lights: instead of using 5 PLC outputs, you use one communication port on the PLC, send a single command like “turn channel 2 (yellow) on, channel 3 (green) off, buzzer pulse once” and done. No more burning PLC outputs, less wire clutter, easier to tweak later.
But wait—your PLC needs to play nice with RS485, right? That’s where most people get stuck. A lot of basic PLCs have Ethernet or discrete I/O, but not a native RS485 port. Common PLC brands like Siemens, Allen-Bradley, Mitsubishi all have modules or adapters that add RS485 capabilities. For example, if you have an Allen-Bradley CompactLogix, you can pick up a 1747-DCM module that turns one of its serial ports into RS485. If you’re using a cheap, entry-level PLC for a small machine, don’t worry—there are USB-to-RS485 adapters too, we even test these with our lights all the time. Just make sure the PLC supports Modbus RTU, because that’s the protocol almost all RS485 stack lights (including ours) use. Modbus is like the universal language for industrial serial devices—your PLC already knows how to talk Modbus, or at least has a library you can import in the programming software.
Here’s a real example to make this concrete. Last month, a customer in the food packaging industry bought 8 of our 3-color RS485 stack lights for a new shrink-wrap line. Their PLC was a Siemens S7-1200, which had a Profinet port but no native RS485. We suggested a cheap Profinet-to-RS485 gateway adapter—like, $60 on Amazon, super simple to set up. They wired the gateway to their PLC, connected the RS485 A and B wires from each stack light to the gateway, powered everything, and were up and running in 2 hours. Before that, their old relay-based stack lights used 8*3=24 PLC outputs, which they didn’t have room for. Now, they use one gateway and one set of comm wires for all 8 lights. No extra hardware, no headaches.
Now, let’s talk about the gotchas, because this isn’t all sunshine and rainbows. First, network sizing. RS485 networks have limits. Total cable length can’t exceed 1200 meters (that’s 3937 feet, for the metric folks, but in industrial settings, you rarely need that long). Number of devices maxes out at 32, including the gateway and any other RS485 devices you might have (like temperature sensors or motor drives). If you need more than 32, you can add a repeater, but that’s a extra step most people don’t plan for upfront. Second, addressing. Each RS485 stack light needs a unique address, right? Because if two lights have address 1, your PLC will send a command to address 1, and both will light up, which is not what you want. Our lights have tiny DIP switches on the back—you set 1 to 31, easy. No software needed, no manual programming for each light, which is a huge time-saver. Third, termination resistors. This is the part that makes people call us at 9 PM panicking because their lights flicker randomly. RS485 networks need a 120-ohm termination resistor at the very first and very last device on the network. If you skip that, you get signal reflections, which cause garbled data, intermittent light issues, or no communication at all. Our stack lights have a jumper on the inside to toggle the termination resistor—just flip it on for the first and last light in your chain, off for all the middle ones. Super simple, but if you miss that, you’re gonna have a bad time.
Wait, can you connect RS485 stack lights directly to a PLC without an adapter? Let’s clarify that. If your PLC has a native RS485 port (like some older Mitsubishi FX series PLCs), yes, you can wire the RS485 A and B from the light straight to the PLC’s RS485 terminals. No extra hardware needed. But most newer, more common PLCs don’t have RS485 built-in, so you’ll need a module, adapter, or gateway. We make a setup guide for every single one of our stack lights that lists compatible PLC modules and common gateways, so you don’t have to Google for hours like we did back in the early days.
Another common question: what about if I only need one light, not a whole network? Can I connect it to my PLC? 100% yes. It doesn’t matter if you have 1 light or 30—RS485 works for single-device setups too. You can even test a single light with a cheap USB-to-RS485 adapter and your laptop before you deploy it, which is how we debug every light that comes back for warranty. That’s a big plus for small machine builders or hobbyists who don’t want to drop thousands on a fancy PLC just for a stack light.
Let’s compare this to the old way, because that’s where the value hits. Old discrete stack light setup: 5 lights = 5 outputs, plus wire, plus labor to run all that wire. If you need to move the light later, you have to re-terminate 5 wires, find a new PLC output, etc. RS485 setup: one set of two wires for all lights, re-address a light in 10 seconds if you move it, no extra outputs. For our customers, that’s cut wiring time by 70% on average, per our surveys last year. One customer in automotive assembly told us they saved $1,200 on PLC output modules for a 12-light line because they went RS485. That’s real money, not just tech hype.
Now, let’s talk about reliability, because industrial environments are harsh—dust, heat, vibration, voltage spikes. Our RS485 stack lights are rated IP65, so they can take being hosed down with water if you’re in a food or beverage plant. RS485 is differential, so it’s way more immune to EMI (electromagnetic interference) from motors or welders than old 0-10V or discrete wiring. We’ve had customers run RS485 networks next to 480V motor cables for 2 years with zero communication issues, which is a game-changer in tight industrial spaces.
Wait, what about if my PLC only has Ethernet? No problem, like I mentioned earlier, Ethernet-to-RS485 gateways are super cheap and easy to set up. You just assign the gateway an IP address, map the Modbus registers from the gateway to your PLC’s tags, and you’re good to go. Our setup guides even have step-by-step for Siemens TIA Portal, Allen-Bradley Studio 5000, and even free software like Ignition SCADA if you’re using that. We’ve had hobbyists connect our lights to Arduino or Raspberry Pi too, but this question is about PLCs, so let’s stay on topic.
The only time you might have an issue connecting an RS485 stack light to a PLC is if you skip the basics: not checking Modbus protocol compatibility, forgetting the termination resistor, or not setting unique addresses. We get at least 5 calls a month from people who messed up one of these three things, and we walk them through it in 10 minutes. For example, last week a customer from a metal stamping plant called because his lights kept flickering. We asked if he had termination resistors on the first and last light—he said no, he thought they weren’t needed for a small network. We told him to flip the jumpers on the end lights, and he texted us 5 minutes later saying it worked. That’s not a stack light flaw, that’s a network 101 mistake that’s easy to fix.
So to wrap this up: Yes, an RS485 stack light can absolutely be connected to a PLC. It’s not only possible, it’s often the better, more cost-effective option than old discrete setup, as long as you: 1) Make sure your PLC supports Modbus RTU, or add a simple adapter/gateway if it doesn’t have native RS485, 2) Assign unique addresses to each light, 3) Add 120-ohm termination resistors at the ends of the network.
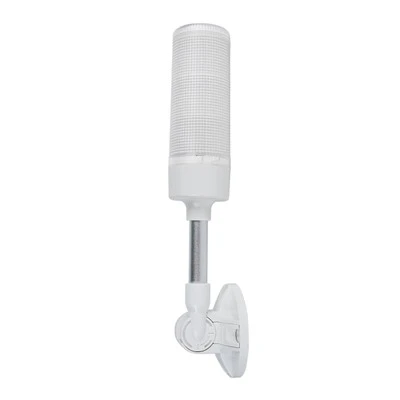
If you’re in the market for RS485 stack lights, or you have a setup you’re trying to get running and need a hand, we’re here to help. We’ve worked with thousands of customers across manufacturing, automotive, food and beverage, and more, so we can help you pick the right light size, color options, and compatible hardware for your PLC. No pushy sales stuff, just real advice from people who build and use these lights every day. Reach out to our team to chat through your setup and get all your questions answered.
LED Gooseneck Light References:
- Industrial Serial Communication Basics: RS485 and Modbus, Automation Direct, 2022
- Stack Light Integration Guides for PLCs, Banner Engineering, 2023
- RS485 Network Design Best Practices, Rockwell Automation, 2021
Suzhou Pouge Lighting Electrical Appliance Co., Ltd.
As one of the most professional rs485 stack light manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale advanced rs485 stack light made in China here and get quotation from our factory. For price consultation, contact us.
Address: Building 6-501, No.1330, Jinfeng South Road, Mudu Town, Wuzhong District, Suzhou City, China
E-mail: xduanlyy@126.com
WebSite: https://www.pouge-light.com/
