If you’ve ever stood next to a steam turbine, gas turbine, or even a large industrial hydro turbine humming at full capacity, you know how critical that piece of machinery is to keeping a plant running smoothly. But what many people don’t see is the work happening behind the scenes to keep the turbine’s oil clean, cool, and functional—work done by a turbine oil purifier. As someone who’s been supplying these systems for over 12 years, I’ve talked to hundreds of plant engineers and maintenance managers who ask the same question: how exactly do these purifiers turn dirty, degraded turbine oil back into a fluid that protects the turbine’s expensive components? Turbine Oil Purifier
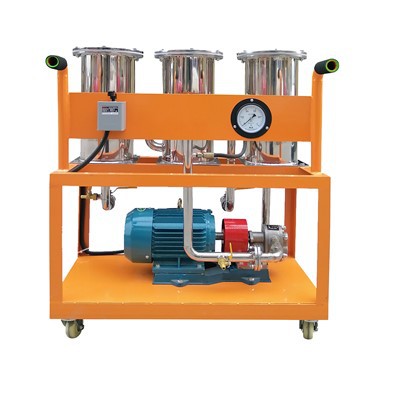
I get it. When you’re managing a plant that runs 24/7, you don’t have time for trial-and-error when it comes to your oil treatment. You need methods that are proven, efficient, and tailored to your specific turbine’s needs. Over the years, I’ve seen a lot of myths and misconceptions about turbine oil purification—some people think it’s just filtering out big gunk, but modern purifiers handle everything from tiny water droplets dissolved in oil to the chemical breakdown products that make oil turn acidic and sludge-like. Today, I want to break down the core control methods that turbine oil purifiers use, and share some of the lessons I’ve learned from working with plants across different industries.
First, let’s start with the basics: what’s in dirty turbine oil that we need to remove? Turbine oil works under extreme pressure and heat, so it picks up contaminants over time. These fall into a few main categories: solid particles (metal wear debris, dust, rust), water (from condensation during shutdowns or leakage into the system), and oxidation byproducts (acids, varnish, sludge from oil breaking down). A good purifier doesn’t just target one of these—it addresses all three, using a combination of control methods that work together seamlessly.
One of the most common and foundational control methods is mechanical filtration. If you’ve used a filter at home for dirty water, you get the idea, but industrial turbine oil filtration is way more precise. It’s not just a mesh screen; we use different filter grades depending on the size of particles we’re targeting. For most turbine systems, we use depth filters—these are made of materials like cellulose, polyester, or polypropylene that have tiny, porous structure. As oil flows through, particles get trapped deep in the filter material, not just on the surface. That’s important because surface filters can clog fast and reduce flow, which slows down the purification process.
But mechanical filtration isn’t one-size-fits-all. We control it using particle counters integrated into the purifier system. These devices measure the number and size of solid particles in real time, usually down to 1 micron (that’s 1/100th the width of a human hair). If the particle count gets too high—like if a turbine just had maintenance and metal debris got into the oil—the system automatically adjusts the flow rate through the filters. It slows down to give the filters more time to catch small particles, and when the filters are nearing their capacity, the control unit alerts operators to replace them before they clog. I always tell my clients that this real-time control cuts filter replacement costs by 30% on average, because you’re only changing filters when they actually need it, not on a rigid schedule.
Next up, water removal—this is a huge one because even tiny amounts of water in turbine oil cause big problems. Water can reduce oil’s lubricating properties, cause corrosion on turbine shafts and bearings, and speed up oil oxidation. Most plants think they can just drain water from the oil sump, but dissolved water (water that’s mixed into the oil so you can’t see it) is the tricky part. The main control method for removing this is vacuum dehydration. Here’s how it works: the purifier heats the oil slightly (usually to 120-140°F, not hot enough to damage the oil) and then sprays it into a vacuum chamber. The vacuum lowers the boiling point of water, so it turns from liquid into vapor at a much lower temperature, separate from the oil. The vapor is then condensed and removed from the system.
But controlling vacuum dehydration isn’t just about turning on a vacuum pump. We use multiple sensors to keep everything stable. A temperature sensor monitors the oil entering the vacuum chamber—too hot and you’ll start breaking down the oil, too cold and water won’t evaporate. A vacuum gauge keeps the chamber at exactly the right pressure, usually around 29 inches of mercury, which is enough to evaporate water without wasting energy. Some of our more advanced systems also have a dew point sensor that checks the moisture level in the vacuum vapor, adjusting the vacuum or heating to make sure you’re not leaving any water behind. I remember a client at a coal plant in Pennsylvania who was having consistent issues with water-related bearing failure. After installing a purifier with this automated vacuum control, they reduced bearing failures by 80% in six months. That’s the kind of result that makes this control method worth investing in.
For plants that handle larger volumes of oil or have higher water contamination, there’s another control method called coalescence-separation. Coalescence works by bringing tiny water droplets together into larger ones. The oil flows through a coalescer element—usually a material with small fibers that attract water. As small droplets hit the fibers, they stick and merge into bigger droplets that are heavy enough to sink. Then, the oil flows into a separator chamber where the separated water settles at the bottom and is drained off. The control here is all about the flow rate through the coalescer. If you push oil too fast through the coalescer, the droplets don’t have time to merge; if you go too slow, you’re wasting time and energy. Modern systems use a flow meter paired with a control valve to adjust the flow automatically, based on the inlet water level. This is especially useful for turbines that go through frequent start-stop cycles, which cause condensation spikes in the oil.
Now, what about the gunk that’s not solid or water—varnish and oxidation byproducts? These are the silent killers of turbine oil. Varnish is a sticky, resin-like substance that forms when oil oxidizes, and it coats turbine valves, seals, and control systems. It can make valves stick, reduce efficiency, and even cause unplanned shutdowns. For this, we use adsorption, a control method where the oil passes through a bed of specialty adsorbent materials, like activated alumina or Fuller’s earth. These materials attract and hold onto the acid molecules and varnish precursors, removing them from the oil.
The control for adsorption is a bit trickier than filtration or dehydration because adsorbents don’t work forever. As they absorb contaminants, they get saturated. That’s why we use online acid number (AN) sensors, which measure the level of acidity in the oil. The acid number is a standard metric—for turbine oil, you want an AN below 0.2 mg KOH/g. When the AN starts to rise above that threshold, the purifier’s control system signals that it’s time to replace the adsorbent bed. Some of our systems even have a bypass control: if the adsorbent is nearing saturation, the oil flows through a smaller bypass line so you can continue purifying while you change the adsorbent, without taking the whole system offline. That’s a huge benefit for plants that can’t afford any downtime.
Wait, I should also mention the integrated control system that ties all these methods together. A turbine oil purifier isn’t just a collection of filters and pumps—it’s a centralized control unit that manages every part of the process. This is where a lot of lower-quality purifiers fall short. Some use manual controls, where an operator has to adjust valves and check gauges every hour, which is prone to human error. Our purifiers use PLC (programmable logic controller) systems that connect all the sensors: particle counters, moisture sensors, temperature gauges, acid number meters. The PLC uses pre-programmed algorithms to adjust every parameter in real time. For example, if a sudden spike in solid particles is detected, it increases the flow through the filtration system; if the vacuum chamber’s temperature drops, it turns up the heating element slightly. The system also logs all the data, so maintenance managers can track oil quality over time and plan maintenance before issues arise.
I often get asked: what’s the biggest mistake plants make when it comes to purifier control? It’s not using the data from the sensors to adjust the system. I had a client at a paper mill in Wisconsin who was using a basic, manual purifier. They’d change the filters every month, regardless of how dirty the oil was, and they were going through adsorbent way too fast. After we installed an automated purifier with real-time control, they found that their filters only needed changing every 10 weeks on average, and adsorbent lasted twice as long. That translated to over $15,000 a year in savings for them—money they could put back into maintenance or efficiency projects.
Another thing I always emphasize is that control methods need to be matched to the turbine’s operating conditions. A gas turbine in a natural gas processing plant runs at much higher temperatures than a hydro turbine in a dam, so its oil is going to oxidize faster and have different contamination levels. That’s why we don’t sell one-size-fits-all purifiers. We work with each client to audit their current oil conditions, their turbine’s operating schedule, and their maintenance goals, then customize the control settings of the purifier to fit their needs. For example, a hydro turbine that runs 24/7 with minimal start-stop might not need as aggressive vacuum dehydration, while a gas turbine that cycles daily needs more frequent moisture removal and adsorption.
I’ve been in this business long enough to see how a well-controlled turbine oil purifier doesn’t just extend oil life—it protects the entire turbine. I’ve seen turbines run 15 years longer than their expected lifespan because their oil was consistently maintained with the right control methods. The cost of a good purifier and its maintenance is a tiny fraction of the cost of replacing a turbine’s bearings or control system.
At the end of the day, turbine oil purification is all about precision control. It’s not just pumping oil through a machine—it’s using real-time data and tailored settings to remove exactly the contaminants you have, when you need to remove them. If you’re dealing with oil-related issues on your turbine, whether it’s water in the system, high particle counts, or varnish buildup, the right purifier with the right control methods can make a huge difference.

If you’re looking to upgrade your current purification system or find a solution that fits your specific turbine’s needs, I’d be happy to talk through your requirements. We’ve worked with plants of all sizes, from small hydro operations to large power generation facilities, and we can help you find a control system that keeps your oil clean, your turbine running smoothly, and your maintenance costs under control. Don’t wait for an unplanned shutdown caused by dirty oil—reach out today to discuss your turbine oil purifier needs.
Fuel Oil Purifier References
- Society of Tribologists and Lubrication Engineers (STLE). (2021). Turbine Oil Filtration and Purification Guidelines. STLE Press.
- American Petroleum Institute (API). (2019). Standard for Gas Turbine Oil Systems, API 614. API Publishing.
- Department of Energy (DOE). (2020). Best Practices for Industrial Turbine Oil Maintenance and Purification. Office of Energy Efficiency and Renewable Energy.
- Hydraulic Institute. (2022). Purification Methods for Industrial Lubrication Oils. Hydraulic Institute Standards.
Chongqing TOP Oil Purifier Co., Ltd.
Chongqing TOP Oil Purifier Co., Ltd. is one of the most experienced turbine oil purifier manufacturers and suppliers in China. Please rest assured to buy CE approved turbine oil purifier made in China here from our factory. We also accept customized orders.
Address: No.1, Jianlong North Rd, Jiulongpo District, Chongqing, China
E-mail: sales@topoilpurifier.com
WebSite: https://www.xboilpurifier.com/
