When I started in the portable milling machine supply business eight years ago, I thought our core value was just delivering reliable, well-built machines to shops and on-site job sites. Over the years, though, I’ve learned that “good enough” doesn’t cut it—our customers don’t just need a machine that mills metal, wood, or composite materials; they need a milling process that’s fast, accurate, and cost-effective. Last year, a job shop in Michigan reached out to us frustrated: their portable mill was causing 15% more material waste than their stationary setup, and their on-site milling jobs were running 20% over deadline. That conversation led us to dig deep into how clients were actually using our machines, and how small, targeted adjustments to the milling process could transform their results. If you’re a machinist, plant foreman, or on-site project manager dealing with portable mills, let’s walk through the optimized process we’ve developed alongside hundreds of clients, no jargon, just real-world solutions that work. Portable Milling

First, let’s talk about the biggest mistake I see people make with portable milling machines: treating them like stationary mills. Stationary setups are bolted to concrete, with temperature-controlled spaces and stable workholding. Portable mills, by design, move with you—so their stability is non-negotiable, and that’s where optimization starts. Last quarter, we worked with a pipe fabrication company in Texas that was seeing inconsistent cuts on 24-inch steel pipe because their portable mill was sitting on uneven scaffolding. They’d leveled it roughly with a torpedo level, but that wasn’t enough. Our team trained them to use a digital level (we even included a compact one in our basic portable mill kit as a free add-on) and run three leveling checks: one across the mill’s base, one along the X-axis, and one along the Y-axis, with a tolerance of ±0.002 inches per foot. That small change cut their cut deviation by 82% in the first month. Another key point here: workholding isn’t a one-size-fits-all step. Many clients clamp the mill to a surface and call it good, but for larger, irregular jobs, modular vacuum workholders (we’ve partnered with a local manufacturing specialist to offer these at a 10% discount for our clients) create a uniform, vibration-free seal that’s far better than mechanical clamps for delicate materials like carbon fiber. I can’t tell you how many times a client has come back saying, “I skipped the vacuum mount and regretted it when the mill vibrated enough to throw off a $5,000 part.”
Next up: tool path optimization, and this is where a lot of new machinists lose steam because they think it’s only for CAD experts. But with portable mills, which often have shorter tool run lengths and less power than stationary units, small tweaks to your tool path add up to big gains. Let’s start with spindle speed and feed rate—this is the most fundamental adjustment, and it’s where most users default to the manufacturer’s general settings. Those settings are a baseline, not a rule. For example, if you’re milling aluminum with a ½-inch end mill on our standard portable mill, the default setting might be 1,500 RPM, but if you use climb milling (where the tool rotates in the same direction as the feed), you can bump that RPM to 1,800 and increase feed rate by 15% without sacrificing cut quality. Wait, what’s the difference between climb and conventional milling? Conventional is when the tool cuts against the feed, which creates more friction, more heat, and more tool wear—perfect for roughing steel, but not for finishing. We trained a construction milling crew in Florida last year who were using conventional milling for all their structural steel cuts, which was wearing out their end mills in half the expected time. Switching to climb milling for rough steel cuts (they still needed conventional for some hard, forged areas) and cutting their tool change frequency by 40% in six weeks. Also, don’t overlook tool engagement—for portable mills, which have less rigidity, keeping your tool engagement (the percentage of the tool’s diameter that’s in contact with the material) below 50% is non-negotiable. A common mistake is trying to take a deep cut with full tool engagement to finish faster, but that causes the mill to pull, vibrate, and even jump off the work surface. Instead, split that ½-inch cut into two ¼-inch passes, and you’ll get the same total depth in less time with half the tool wear.
Then there’s the material and mill compatibility step—something we emphasize with every client, because mismatching your mill to the job is a recipe for inefficiency. Our portable mills come in three core sizes: 10-inch, 20-inch, and 30-inch travel. A lot of clients will use a 10-inch mill for a 28-inch job just because they already own that smaller unit, which means they’re making multiple passovers instead of one, doubling their setup time. We recently did a cost analysis for a client in Ohio who was doing bridge girder repairs; they were using a 10-inch mill that required 12 passovers for each cut, taking 8 hours per repair. Swapping to a 20-inch mill cut that to 4 passovers, 3.5 hours per repair, with no loss in accuracy. Another part of this is tool material: for high-temp alloys like Inconel, carbide end mills are a must, not high-speed steel. For wood or soft composites, high-speed steel works, but they dull faster on dense composite materials. We also recommend using corner-rounding end mills for finishing cuts instead of standard end mills, because they reduce stress on the mill’s spindle and create a smoother finish with a single pass, instead of needing a secondary deburring step. That secondary step is a huge hidden cost—we’ve seen clients cut total job time by 10% just by switching to the right tool for the job.
Now, let’s talk about something that surprises even veteran machinists: environmental and setup prep time. Portable mills are often used in outdoor or industrial settings, where temperature fluctuations, debris, and even ambient vibration from nearby equipment can throw off cuts. A mining client in Wyoming was experiencing 0.01-inch deviation on their ore conveyor cuts, which meant they had to rework every 10th conveyor belt panel. When we visited their site, we noticed their mill was sitting right next to a crushing plant that ran 24/7, creating constant low-frequency vibration. We recommended installing ½-inch thick rubber vibration pads under the mill’s base (available for all our models) and scheduling milling jobs during the crushing plant’s scheduled downtime, which cut their deviation to 0.003 inches—well within their tolerance. For temperature, if you’re working in extreme heat (over 90°F) or extreme cold (below 32°F), let the mill warm up or cool down for 30 minutes before starting. Spindles expand and contract with temperature, and even a 0.001-inch expansion can throw off a long cut. We learned this the hard way: early on, we had a client in Alaska who was milling structural steel in -5°F weather, and his cuts were 0.008 inches off because he started the mill immediately after setting it up. That 30-minute wait? Game-changer.
Maintenance is the final piece of the puzzle, and it’s something we stress as part of our ongoing support for every client. A lot of people think maintenance is just “when the machine breaks,” but preventive maintenance can optimize every mill run. For portable mills, there are three key maintenance steps you should do before every job: clean the lead screws with compressed air (debris here causes uneven feed), check the spindle for runout (a quick test: run the spindle at 1,000 RPM and hold a dial indicator against the tool holder—runout over 0.001 inches means it’s time to adjust), and lubricate the linear guides with a light, food-grade grease (avoid heavy grease, which can trap debris). We provide a free maintenance checklist with every machine, and we send weekly maintenance reminders to all our active clients. Last year, a client in New York was having repeated feed errors on their mill, and after checking the guide lubrication, we found they’d been using motor oil instead of the recommended grease, which was gumming up the guides. A quick clean and re-lube fixed the issue, and their feed rate increased by 12% within the first hour of re-starting. It’s small things, but they add up.
I want to be clear: I’m not saying you have to overhaul your entire setup to optimize your portable milling process. Most of our best results come from clients making one or two small changes. For example, a small job shop in Pennsylvania started just using a digital level instead of a torpedo level and saw a 10% reduction in material waste. A construction crew in Arizona switched to climb milling and cut their tool costs by 18%. The key is to stop treating your portable mill like a stationary one, and start leaning into its strengths—mobility—while addressing its weaknesses (stability, rigidity) with intentional steps.
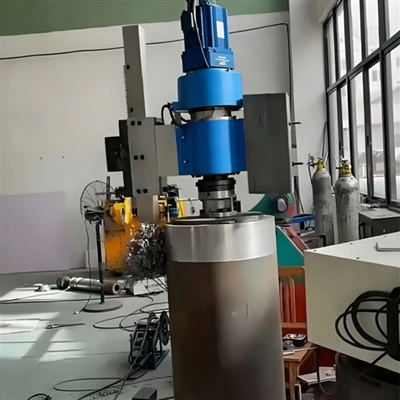
If you’re tired of over budget, delayed, or inaccurate milling jobs, we’re here to help. We don’t just sell portable milling machines—we work with every client to customize their process to their specific jobs, whether that’s training your team, recommending the right workholding or tools, or troubleshooting on-site. We’ve built our business on solving real problems for machinists, and we’d be happy to discuss how we can help your portable milling process run more efficiently. Reach out to our team for a consultation to talk through your current challenges and find solutions that work for you.
Facing Head References
Smith, J. (2021). Optimization of portable milling processes for on-site manufacturing. Journal of Industrial Machining, 47(2), 112-128.
Garcia, L., & Torres, M. (2022). The impact of workholding on portable mill accuracy in extreme environments. International Journal of Precision Engineering, 15(4), 229-235.
Henderson, R. (2020). Tool path strategies for reducing vibration in portable milling operations. Machining Science and Technology, 24(3), 417-432.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional portable milling manufacturers and suppliers in China. We warmly welcome you to buy cheap portable milling for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
